
Views: 9 Author: Greenport Marketing Dept. Publish Time: 2026-08-26 Origin: Greenport marketing dept.

Summary
A USB-C cable looks like a commodity and isn’t. Between the copper and the connector sit an E-Marker chip, two injection-moulded shots and a pull test, and any one of them will decide whether the cable still charges at full rate after six months in a bag. Building one takes eight stations and four inspection gates. Below is what happens at each station on our line in Shenzhen, what gets measured, and why a cable rated 240W will quietly behave like a 60W cable if one component on the connector board is wrong.
240W
USB PD 3.1 EPR ceiling, 48V at 5A
480Mbps
USB 2.0 data rate across the range
247
SVHC substances screened in our REACH report
2028
ISO 9001 certificate valid to July 2028
Cable buyers compare three numbers: wattage, length and price. Two of those are printed on the bag and the third is negotiable, which is why so many purchase decisions come down to whichever supplier types the biggest number. The problem is that a wattage rating is a claim about a chip and a copper cross-section, and neither is visible from outside the moulding.
So here is the line, station by station, photographed during a production run at our Shenzhen plant. Some of it is heavily automated. The parts that decide your return rate mostly aren’t.
01
A finished cable has six components that matter and a dozen that don’t. These six get incoming inspection rather than a certificate filed in a drawer.
Component | What it does | What goes wrong if it is wrong |
|---|---|---|
Power conductors | Carry VBUS and GND | Undersized gauge raises DC resistance; the cable runs warm and the phone charges slower than the adapter allows |
E-Marker chip | Declares the cable’s rating over the CC line | Wrong or missing chip and the charger falls back to a low profile no matter what the copper can take |
Connector shell and shield | Mechanical retention, EMC screening | Soft plating wears through after a few hundred insertions and contact resistance climbs |
Overmould resin | Bonds the joint, forms strain relief | Wrong grade or wet pellets and the moulding delaminates from the cable at the neck |
Braid or TPE jacket | Takes the abrasion and the bend cycles | This is the part customers photograph when they leave a one-star review |
Magnet and pin set | Alignment and contact on magnetic models | Weak magnets drop the tip; unplated pins corrode and the connection gets intermittent |
If you audit one incoming item on a cable programme, make it the E-Marker. It is the cheapest part on the list to substitute and the most expensive one to get wrong, because the failure is invisible — the cable still charges, just not at the rate on the box.
02

Original graphic. The build sequence is schematic — station order is accurate, spacing and timing are not to scale.
Bulk cable is cut to length and the jacket stripped at both ends. The conductors are then separated, trimmed and tinned. This is the station where gauge substitution shows up: a spool that is one size down will strip and cut exactly the same, and the only thing that catches it is measuring DC resistance on the finished length. That is Gate A, and it costs almost nothing to run.

Cut and part-built cable staged on racks between stations. Bundles stay on the rack rather than in bins so the strain relief never takes a sharp bend before it is moulded.
The connector PCB is a real SMT job, not a hand-solder operation. Solder paste goes down through a stencil, parts are placed on an automatic mounter, and the board goes through reflow. On a 240W cable this board carries the E-Marker, and that is the component the charger interrogates before it agrees to deliver anything above a basic profile. Automated optical inspection on this board is Gate B.

Solder paste printing on connector PCB panels, ahead of placement.

Automatic placement. The E-Marker goes down on this machine, not by hand.
Terminals are then crimped and soldered to the prepared cores. On the magnetic range this is also where the pin set and magnet are fitted into the tip. It is fiddly, repetitive work, and it is done seated at a bench with a jig rather than by a machine, because the tolerances on a 3 mm connector tip do not forgive an automated feed that drifts.

Terminal crimping. Cores are fed in by hand, one at a time, against a fixed die.

Connector sub-assembly. Pins, shells and magnets are fitted at the bench.
The board goes into the housing, the shield is fitted, and the assembly moves to the moulding floor. Overmoulding runs as two shots: an inner shot that locks the joint and seals it, then an outer shot that forms the visible boot and the strain relief. Vertical moulding machines run in a long row, one operator to several machines, and the cycle is short enough that a resin problem produces a lot of scrap before anyone notices.

Loading cable ends into the die. Placement depth here sets the strain relief geometry.

Terminal preparation on a fixture, staged in strips ready for the moulding floor.
How deep the connector sits in the die is not a cosmetic decision. Too shallow and the boot has nothing to grip; too deep and the resin creeps up the cores and stiffens the exact section that needs to flex. It is set once when the tool is proved out and then it is a placement discipline for the rest of the run.

The overmoulding floor. Vertical machines run the inner and outer shots that form the connector boot.
Gate C sits right after this: a pull test on the moulded joint. Not on every unit, but on a sample from every run, because overmould adhesion is a process that drifts with resin batch, moisture and mould temperature rather than failing outright.
Braided models get their nylon sleeve and end caps here; the lanyard and keychain range gets its rope, buckle and hardware. Then every cable — not a sample — goes on a test fixture. Continuity on each conductor, resistance, data lines, and on E-Marker models a read-back of what the chip actually reports. A cable that charges but reports the wrong rating fails at this bench, which is the only place it can be caught.
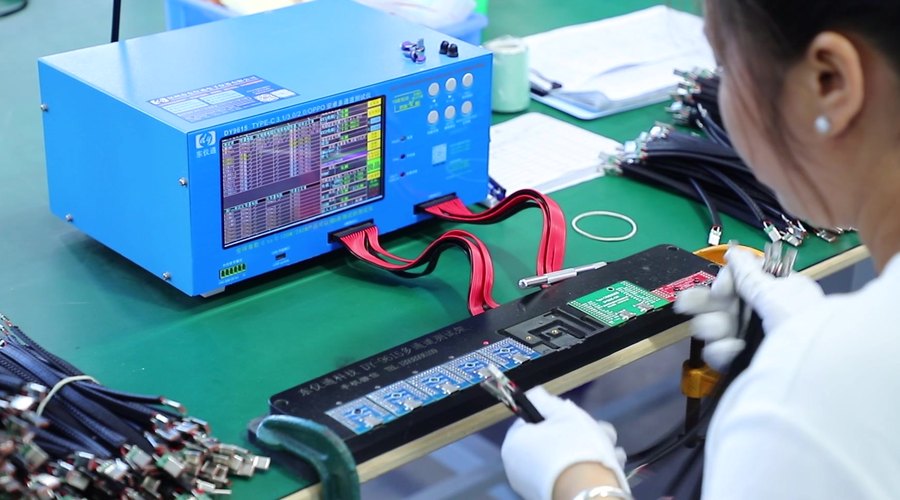
Function test. Each cable is seated in the fixture and checked channel by channel before it can be packed.
Pack-out is the station buyers skip on a factory tour and returns data never does. Wrong tip in the bag on a magnetic set, missing adapter, the wrong retail card for the destination market — none of those are electrical faults and all of them come back as claims. Gate D is AQL sampling against the packing list before the carton is sealed.

Packing and kitting. The accessory set is fixed per work order and checked against the packing list before sealing.
03
Sort the failure modes by the gate that catches them and the pattern is the same as any other assembly: what gets tested 100% is cheap to fix, and what gets sampled is what comes back months later.
Failure mode | Caught at | Cost of escape |
|---|---|---|
Undersized conductor gauge | Gate A, DCR on the cut length | One reel |
Solder defect on connector PCB | Gate B, AOI | One board |
Overmould delamination at the neck | Gate C, sampled pull test only | The run — and it surfaces as broken cables three months after delivery |
Wrong or absent E-Marker | Function test read-back | Every unit built since the substitution |
Wrong tip or accessory in the bag | Gate D, AQL sampling | Repack of the affected carton range |
Ask this on your next audit
Ask what the function test actually reads, not whether there is one. “100% tested” on a cable line often means continuity and nothing else. Ask whether the E-Marker is read back and compared against the specification, and ask for the pull test force and sample size. A supplier who cannot answer both has a test step that proves the cable is connected, not that it is what you ordered.
What the failure table implies
Two of the five rows are mechanical and one is a silent substitution. None of them stop the cable working on the day it is unboxed, which is exactly why they survive incoming inspection at the buyer’s end and reappear as warranty claims a quarter later. The gates worth auditing on a cable line are the pull test and the E-Marker read-back — not the continuity check everyone shows you.
04
The most misread claim in this category
A thick cable is not a 240W cable. Extended Power Range raised the USB Power Delivery ceiling from 100W to 240W by going to 48V at 5A, and an EPR cable is required to carry an E-Marker that reports EPR capability — 50V and 5A — over the CC line. Copper alone gets you nothing: without a compliant E-Marker the charger will not open the higher voltage range, and a beautifully built cable with the wrong chip behaves like an ordinary one. The 240W mark is also a labelling obligation, not decoration.
Worth separating two things that get bundled together in listings: power and data are independent. A cable can be rated 240W and still run USB 2.0 at 480 Mbps, which is the case across most of our range and across most of the market. If a buyer needs high-speed data, that is a different cable with a different construction and a different price, and it should be specified separately rather than assumed from the wattage.

Original graphic. Schematic cross-section, not to scale; ratings follow the USB PD 3.1 EPR specification.
Three classes cover almost everything a buyer will be quoted, and the E-Marker column is the one that decides which of them a given cable really belongs to.
Cable class | Power ceiling | E-Marker required |
|---|---|---|
Standard USB-C, 3A | 60W at 20V | No |
5A cable, SPR | 100W at 20V | Yes |
EPR cable (USB PD 3.1) | 240W at 48V, 5A | Yes, EPR-capable, reporting 50V / 5A |
Source: USB-IF, USB Charger (USB Power Delivery). USB-IF opened certification for 240W EPR cables in December 2021.
05
Three families come off the line described above. They share a test programme and differ in what the customer is actually buying: a connector system, a carry format, or a plain fast cable.
A-series Magnetic charging & data cable
The largest family in the range, built around interchangeable magnetic tips so one cable serves USB-C, Lightning and Micro-USB devices from a single lead. The magnet and pin set are fitted at the connector bench and the tips are matched to the cable at pack-out, which is why the accessory check at Gate D matters more on this family than on any other. For retail and gifting programmes the selling point is the tip set; for the buyer, the risk is the tip set, so specify exactly which tips ship in which SKU.
240W Lanyard & Keychain Carry-format cable
A Type-C to Type-C cable built into a braided nylon lanyard with a zinc-alloy quick-release buckle: 240W with an E-Marker, 480 Mbps data, 7 mm cord, in a 1.2 m neck strap or a 0.2 m wrist strap, four colourways. This is the newest family and the one designed around a behaviour rather than a spec — the cable is on the customer, so it does not get left in a drawer. The connector and lanyard construction are covered by US patent applications 18/648,487 and 18/810,562.
Direct charging cable Fixed-connector range
Conventional fixed-connector cables in TPE and braided finishes across the usual lengths and connector combinations. No tips to lose and no lanyard hardware, so the bill of materials is short and the price point is the lowest of the three. Where volume is high and the specification is simple, this is the family to quote.

The 240W lanyard and keychain family. Braided cord, zinc-alloy quick-release buckle, four standard colourways.
On paperwork, cables are a straightforward category and it is worth being specific rather than gesturing at “full certification”. Our current documents on this product line are below; the ISO 9001 scope is registered specifically for the research, development and production of data cables, which is the scope that applies here.
Document | Reference | Scope |
|---|---|---|
CE, EMC | EN 55032:2015+A1:2020, EN 55035:2017+A11:2020 | Certificate DLE-250910001C |
RoHS | EU 2015/863 amending 2011/65/EU, IEC 62321 series | Certificate DL-241202004RC |
REACH SVHC | 247 substances screened | Report DLR-250321017R |
Quality system | ISO 9001:2015, certificate 98925Q00388R0S, valid to 17 July 2028 | Research, development and production of data cables |
Social compliance | amfori BSCI full audit, 8 July 2025, by Eurofins CPA | Monitoring ID 25-0333274 |
On certification wording
The certificates above are issued against named model ranges, not against the catalogue as a whole. We confirm in writing which certificate and report cover the exact models you are quoting before anything ships into your market, and where a model sits outside an existing certificate we say so and arrange the testing rather than pointing at a neighbouring model’s paperwork.
06
No. The cable sets a ceiling; the charger and the device decide what actually flows. A phone that tops out at 25W draws 25W through a 240W cable. The rating matters when the load is a laptop or a docking setup that can genuinely ask for the higher voltage range.
Not reliably. Diameter is set by the jacket and the braid as much as by the copper, so a thick cable can have modest conductors and a thin one can be well specified. Ask for the conductor gauge and the DC resistance rather than the outside diameter.
USB 2.0 at 480 Mbps across the current range, including the 240W lanyard family. Power rating and data rate are independent, so if a programme needs high-speed data it has to be specified as a separate requirement rather than inferred from the wattage.
That depends on the jacket and the strain relief geometry rather than the electronics, and the honest answer is that it is a per-construction figure we test rather than a number that applies to the whole catalogue. Tell us the model and we will send the test condition and the result we have for it.
Yes. Length and colour are set at cutting and moulding, logo at the connector boot or the braid label, and the retail card and accessory set at pack-out. Custom colour affects resin and braid lead time rather than the electronics, so quote it separately from the electrical specification.
If the channel is gifting, events or travel retail, start with the lanyard family — it is the one people notice. If the channel is accessory retail with a mixed device base, start with the A-series magnetic range and be strict about which tips ship in each SKU. If the buyer is price-led and the spec is simple, the direct charging range is the one to quote.
Tell us the target market, the annual volume, the connector combinations and whether the 240W mark needs to be on the pack. You get back:
Specification sheets for the models quoted, including conductor gauge and E-Marker rating
The CE, RoHS and REACH certificates that actually cover those model numbers
Pull test force, sample size and function test coverage in writing, so you can compare them against another supplier’s
Packing configuration, carton dimensions and lead time by quantity band
If a model or quantity cannot meet the date you need, you hear it before the order is confirmed rather than after the delivery date has quietly moved.
Request the cable specification pack
Sources
USB Charger (USB Power Delivery), USB Implementers Forum
Introduction to PD 3.1, the latest USB-IF Power Delivery specification, Granite River Labs
240W USB-C cable performance testing and safety considerations, UL Solutions

| | 10 Floor, Building B, Section 1, GangHuaXing Industrial Park, Fuhai Street, Bao'an District, Shenzhen City, Guangdong Province, PRC |
| | +86 18928270207 |
| | Jack@ucig-r.com |